
Optical Lens Polishing Machine
Seven machines, one decision. An optical lens polishing machine is chosen by the shape of the surface it has to finish — concave or convex, spherical or flat — and by how many parts you want on the machine at once. Specifications live on each model page; this page is for choosing.
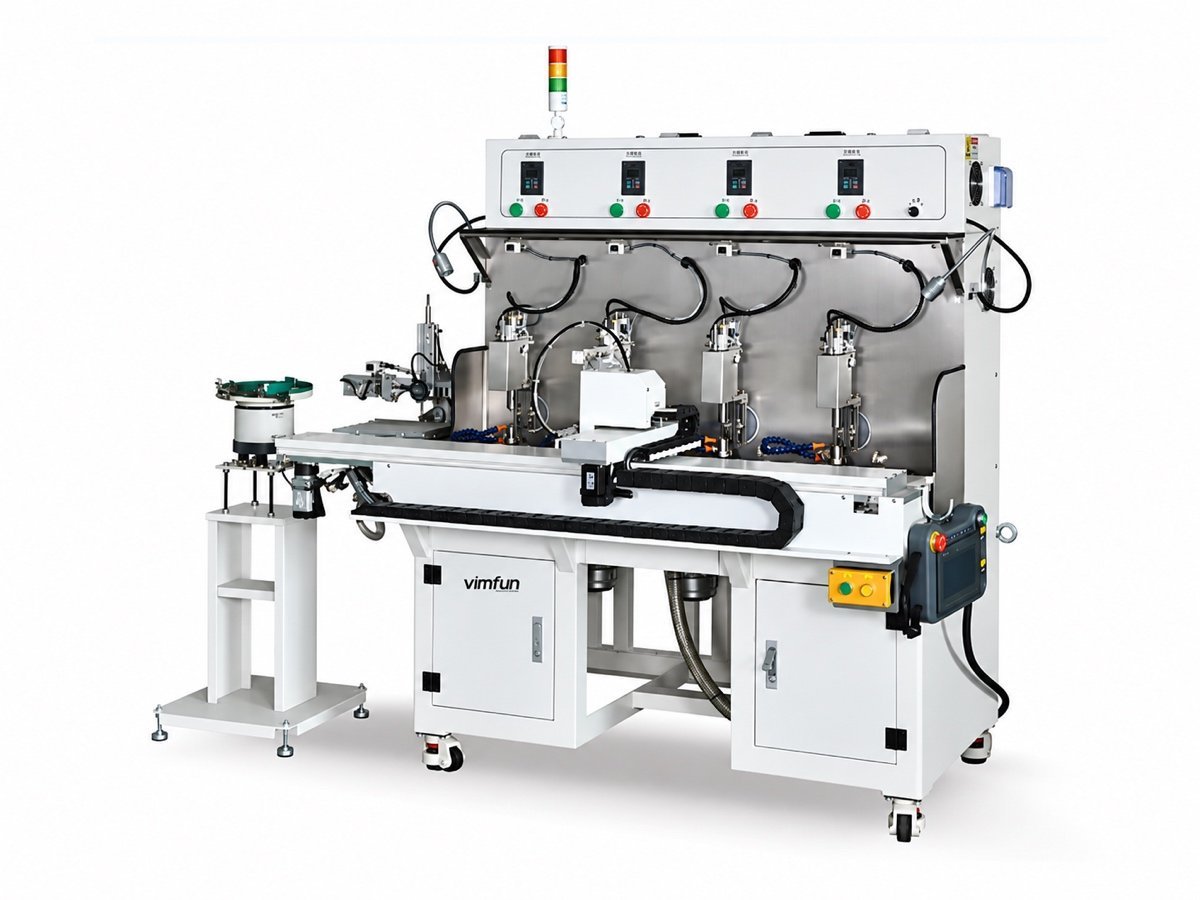
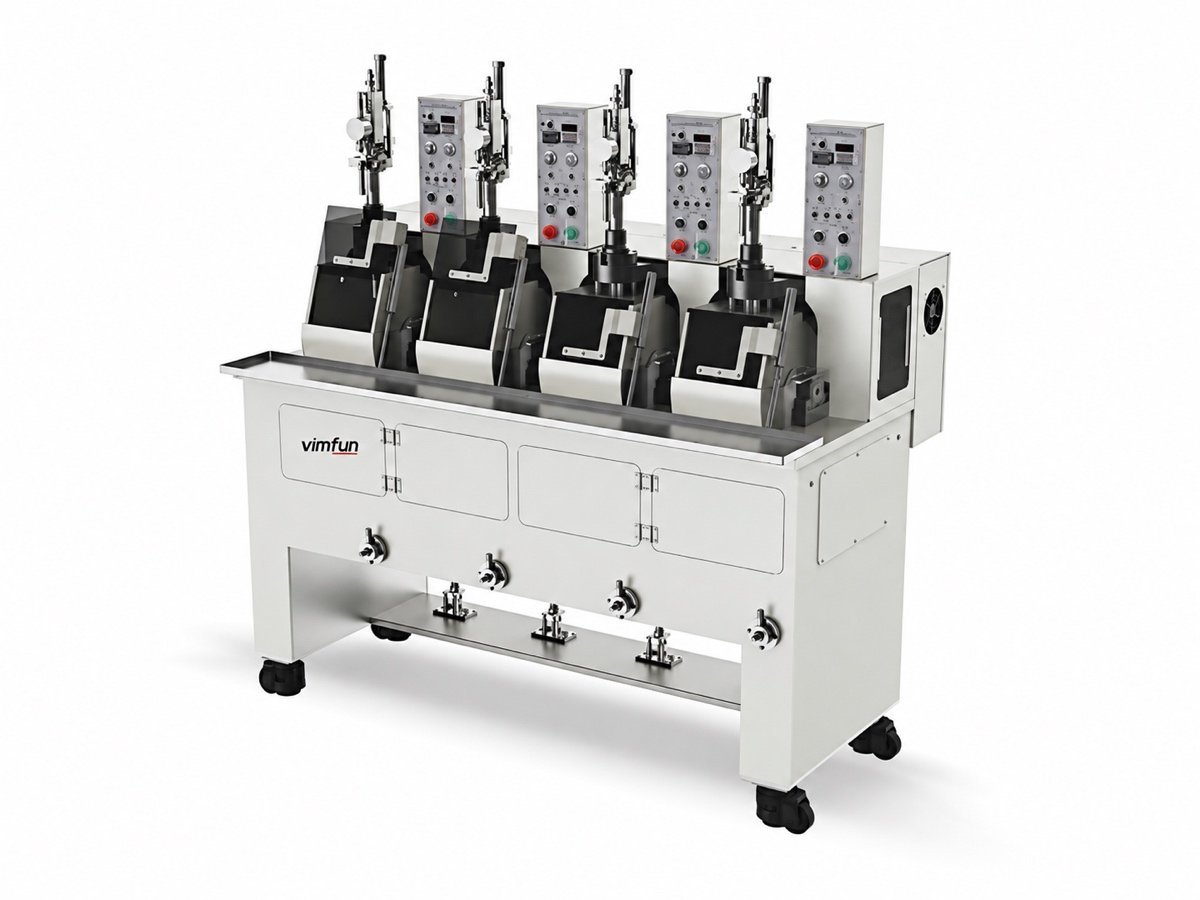
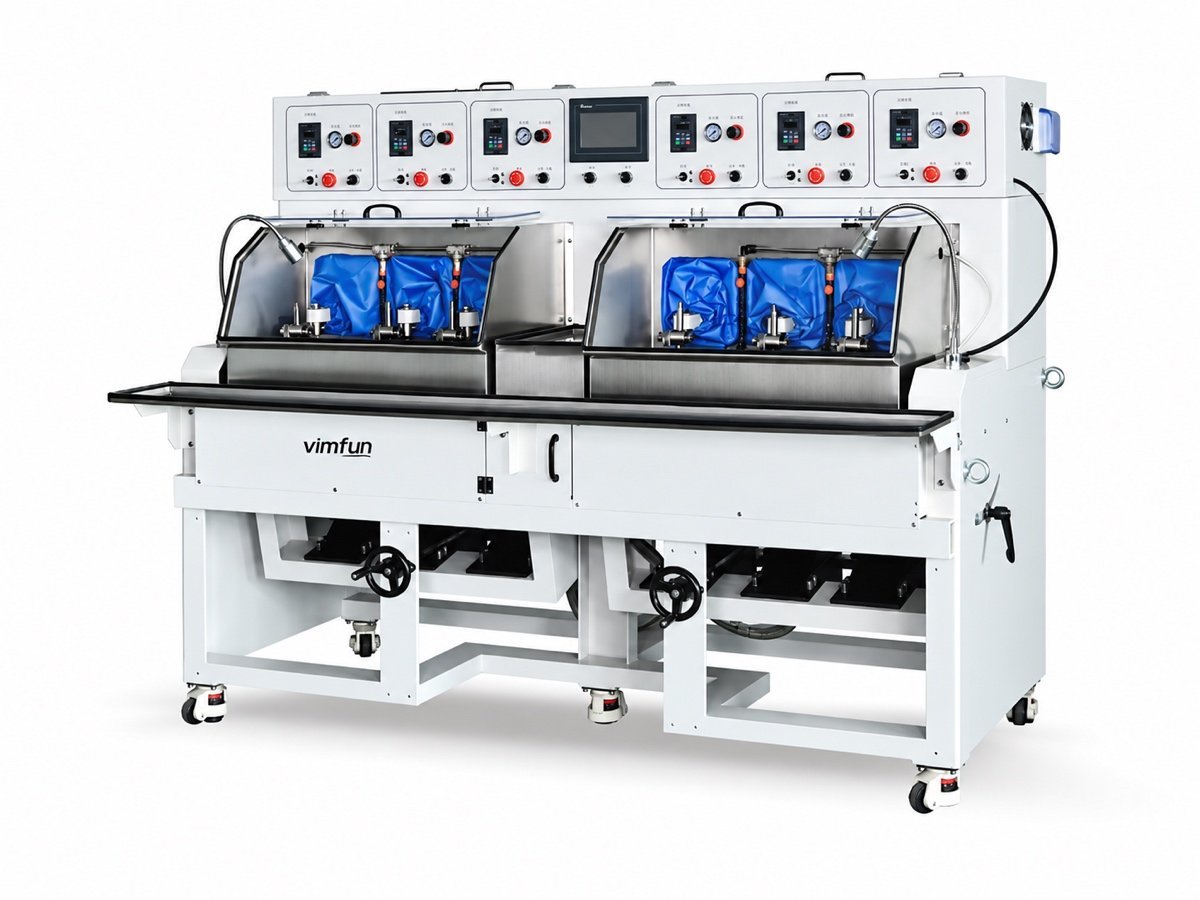
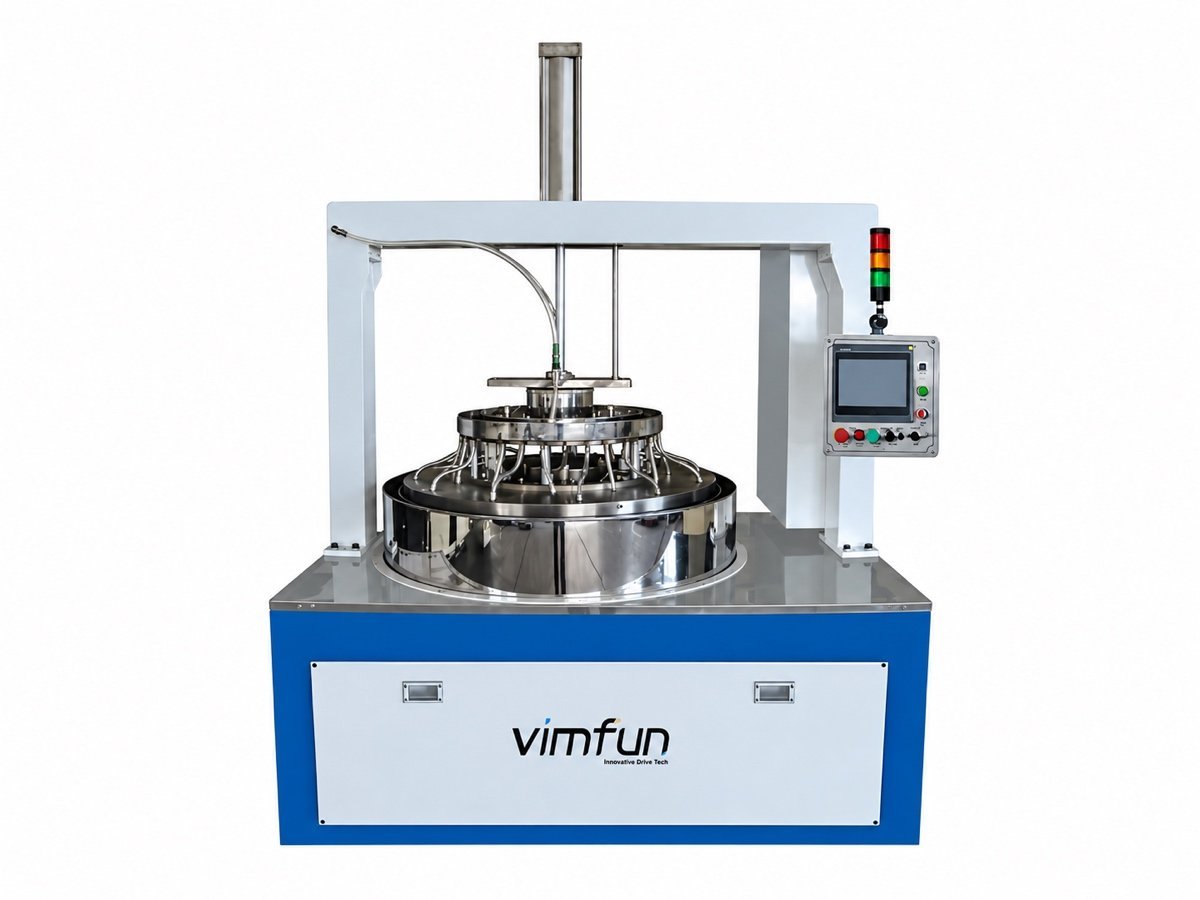
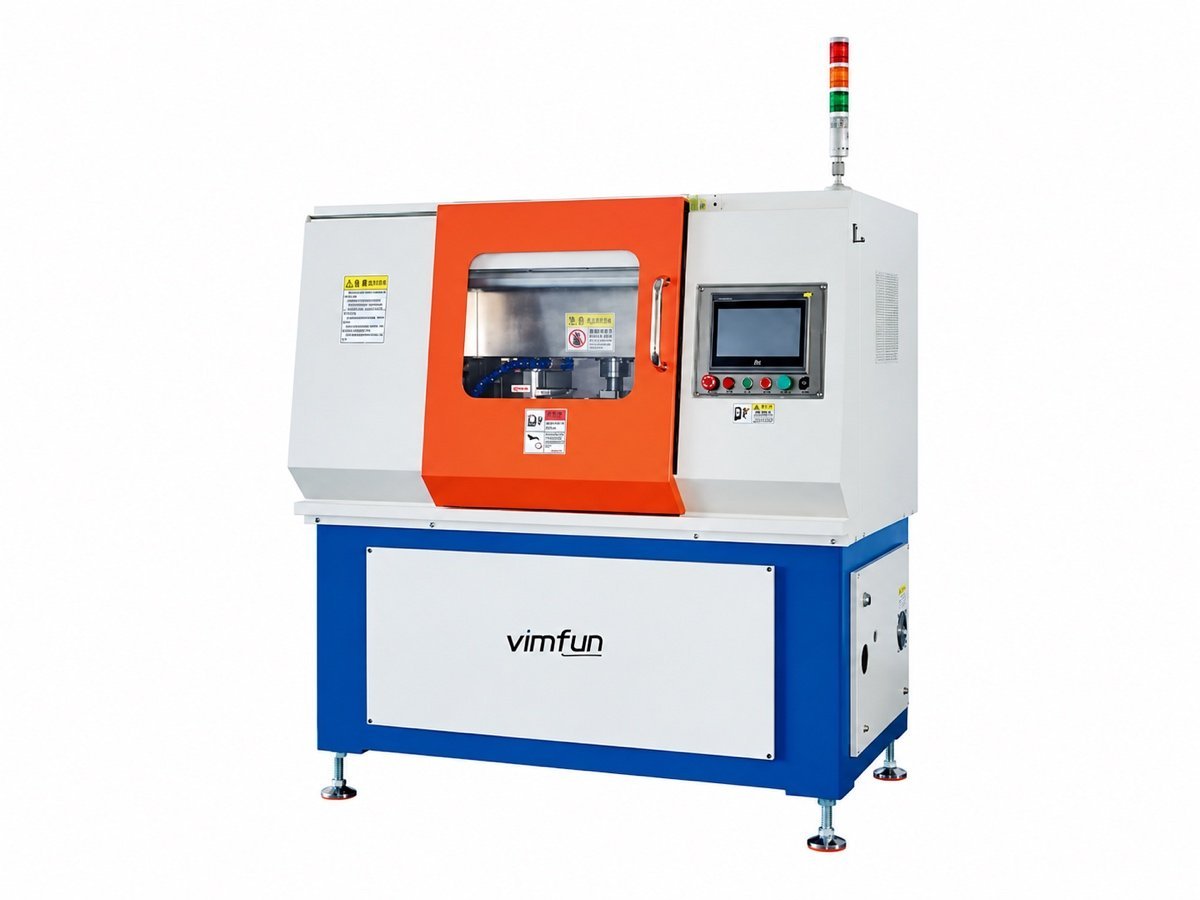
Start from the surface, not from the machine list
Generating leaves a radius with tool marks and subsurface damage. This step removes that damage and brings the surface to its final figure and finish: fine grinding first, with a bonded diamond tool, then polishing with a soft tool and slurry. On this range both jobs run on the same frame — the J and P configurations differ in tooling and consumables, not in the machine bed.
So an optical lens polishing machine is specified from the part, not from a spindle count: the sign of the radius decides the swing direction, the radius value decides the tool and the swing geometry, and the batch size decides how many spindles earn their keep.
Upper swing or lower swing — which way should the lens face?
Swing direction is the first filter and it is not a preference: upper swing is built for concave faces, lower swing for convex. Every optical lens polishing machine below is listed by that split, then by radius and spindle count.
| Model | Principle | Curvature | Diameter | Spindles | Pressure & feed | Choose it when |
|---|---|---|---|---|---|---|
| FP-4U | Upper swing, centre-of-sphere | R1–R20 | ≤ Ø30 mm | 4 | Spring pressure, circulating pump | Concave lenses at small radii — the entry point of the family |
| FP-6U | Upper swing, centre-of-sphere | R1–R20 | ≤ Ø30 mm | 6 | Pneumatic pressure, slurry fed per axis | Same concave work, more output — each axis runs independently of the others |
| FP-4L | Lower swing, centre-of-sphere | ±R1.5–R50 | Ø3–30 mm | 4 | Spring pressure, circulating pump | Convex lenses, and the longest radii in the swing family |
| FP-6X | Tilt axis, −10° to +30° | R10 to flat | Ø10–80 mm | 6 | Pneumatic, peristaltic drip feed as an option | Larger parts, flats and long radii — and ceramics or sapphire, where drip feed matters |
| MF-3 | Indexed layers and facets | Flats and angled facets | ≤ Ø110 mm across, ≤ 30 mm thick | 2 work spindles, 3 plates | Bonded work, CNC plate feed | Prisms and polyhedra — rough, fine and polish on one machine |
| DL-290 DL-395 | Planetary, two plates | Flat, both faces at once | Ø290 / Ø395 workpiece | Batch in carriers | Proportional-valve pressure control | Thickness and parallelism held across a batch rather than part by part |
| EP-220C | CNC contour, two wheels | Perimeter and rounded edges | Ø30–220 mm | 2 polishing wheels | Stacked fixture, CAD outline | The edges of flat 2D and 2.5D panels, not their faces |
EP-220C polishes the perimeter of flat panels. Grinding a lens to its outside diameter, with a chamfer, is a different machine and a different step — see edging and centering.
Radius coverage in the swing family
Four swing machines on one scale. Find your radius, read the swing direction against it, and the shortlist for an optical lens polishing machine is down to one or two frames.
FP-4L carries a ± sign because the lower swing covers both signs of curvature within its range, with convex work as the reason to buy it. An optical lens polishing machine outside the swing family is not on this scale: MF-3 works flats and angled facets, DL laps two flat faces at once, and EP-220C works perimeters — those three are compared further down.
Explore the machine families
One card per optical lens polishing machine: what it is for, and what it is not for. Full specifications sit on the model pages.
FP-4U
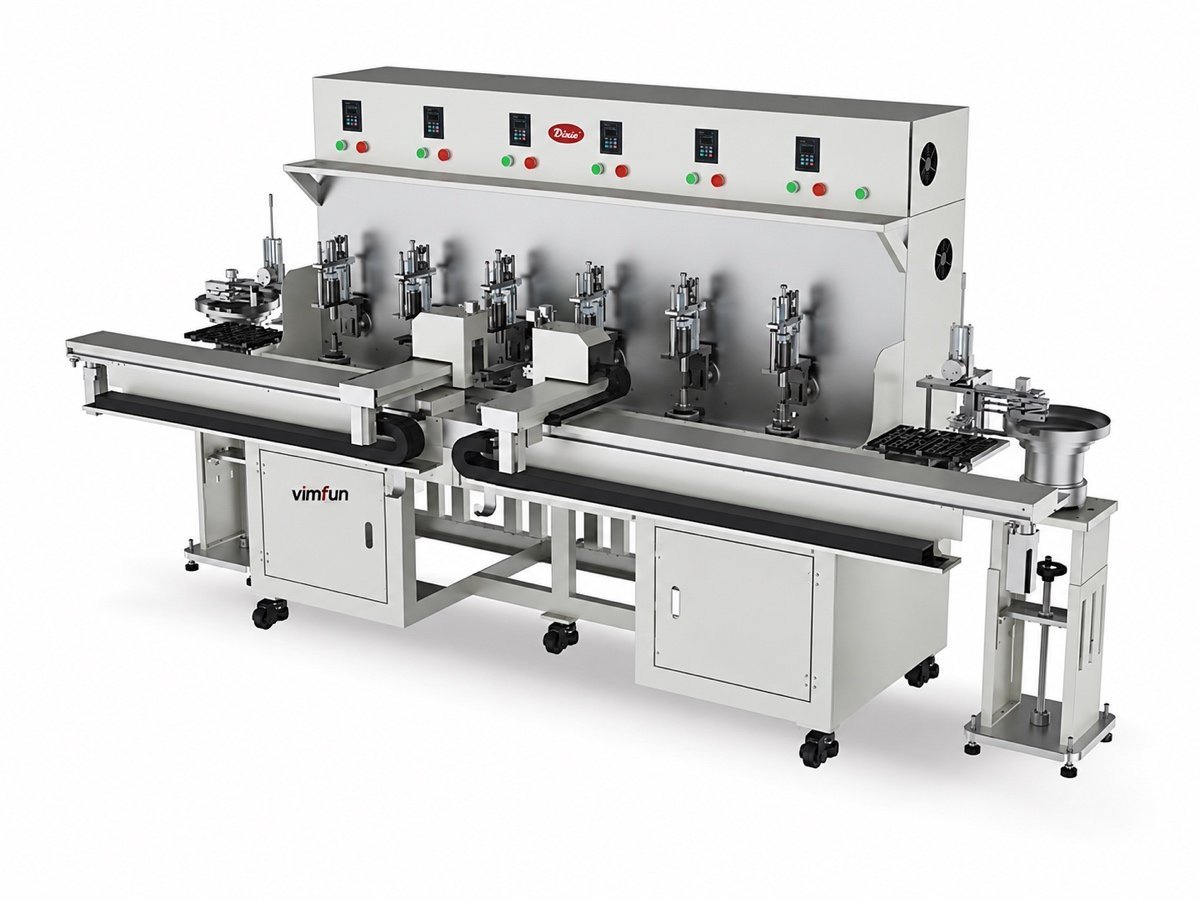
FP-6U
FP-4L
FP-6X
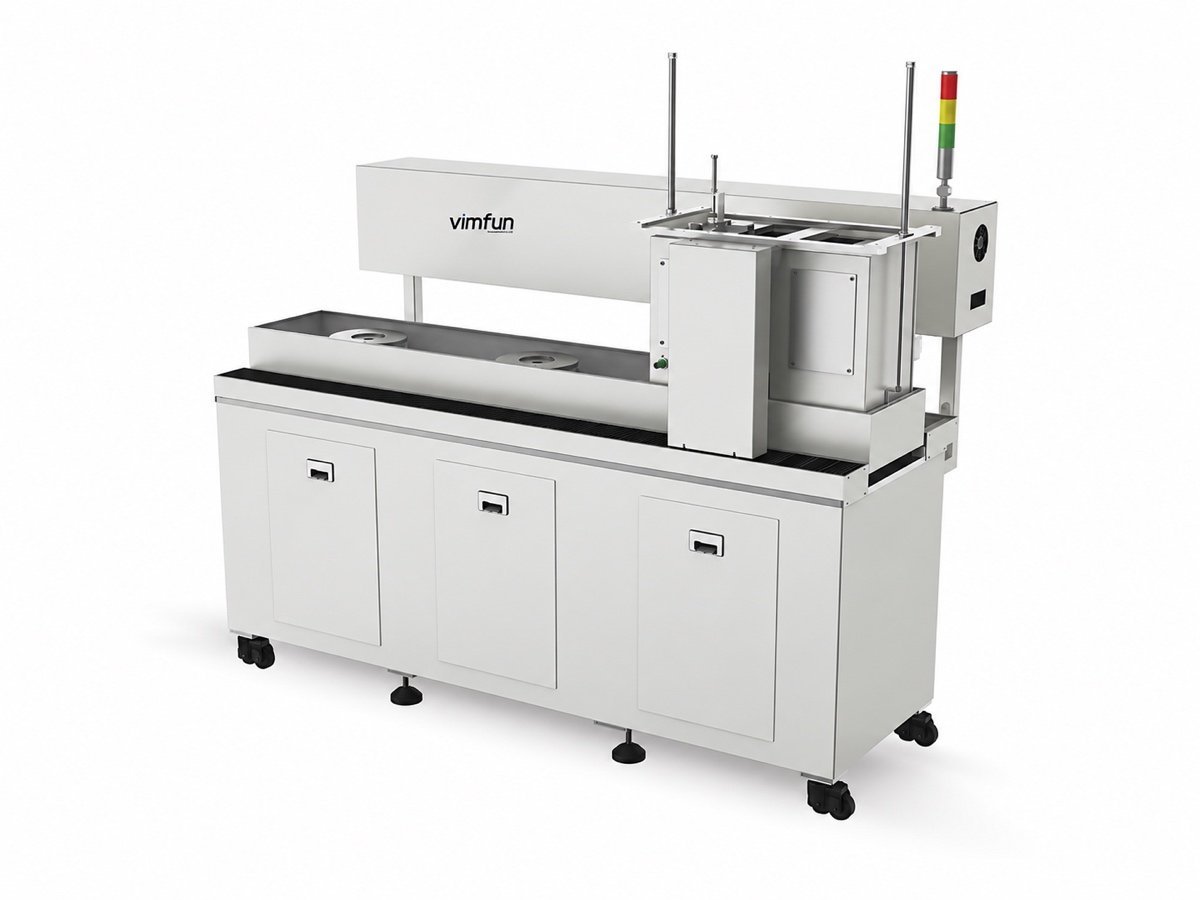
MF-3
DL-290 · DL-395
EP-220C
What actually decides the figure?
Four settings do most of the work on an optical lens polishing machine. Competitors quote spindle counts; these are the things that decide whether the surface comes out round.
The swing runs through the centre of the sphere
Work and tool rock about the sphere's own centre, so the contact path sweeps the whole face instead of wearing a zone. This is why the frame, not the tool, sets what radii a machine can hold.
Stroke and swing speed
Swing rate is set independently per machine — up to 60 cycles a minute on the four-spindle frames, up to 40 and 45 on the six-axis ones. Slower and longer flattens the edge; faster and shorter holds the centre.
How the pressure is applied
Spring pressure on the four-spindle machines, pneumatic on the six. Pneumatic holds a set force as the tool wears, which matters most on long cycles and on parts that will not tolerate a rising load.
How the slurry reaches the interface
Glass runs on a circulating pump. Ceramics and sapphire can be run with peristaltic drip feed on the FP-6X — a metered supply instead of a flood, which is the difference between a stable process and a scratched batch.
Which materials and geometries are covered?
Every optical lens polishing machine here is built for hard, brittle optical materials. Where a specification does not name a material, we prove it with a trial part instead of claiming it.
| Material | Spherical swing | Flat & tilt axis | Double sided | Edge polishing |
|---|---|---|---|---|
| Optical glass | Yes | Yes | Yes | Yes |
| Sapphire | Yes | Yes, drip feed | Yes | Yes |
| Technical and optical ceramics | On request | Yes, drip feed | Yes | Yes |
| Quartz and crystal | On request | Yes | Yes | Yes |
How a material polishes is not one number: hardness, cleavage and thermal behaviour all change the slurry, the tool and the pressure. Published data for sapphire and crystal quartz is a fair starting point; the process is then settled on real parts.
Send a drawing and a few generated blanks of your own material. We run them on the machine under discussion and return the parts with the process sheet — tool, slurry, pressure, swing setting and cycle time. This applies across the range, not only to the machine you first asked about.
Spheres, facets, flats and edges are four different machines
The swing family is only part of this step. Three other groups finish surfaces a swing frame cannot reach, so "optical lens polishing machine" covers four different geometries here. Picking the wrong group is the most common mis-specification we see.
- Spherical faces — the swing family (FP-4U, FP-6U, FP-4L, FP-6X). The tool rocks about the centre of the sphere; radius and sign decide the frame.
- Facets and angled flats — MF-3 indexes the part layer by layer and face by face, and takes it from rough grinding to polish on three plates in one setup.
- Two parallel flats at once — DL-290 and DL-395 lap and polish both faces of flat parts in planetary carriers, holding thickness across the batch rather than part by part.
- Perimeters — EP-220C polishes the edges and rounded corners of flat panels from a stored outline, fed by stacked fixtures.
This equipment is built for precision optics manufacturing. It is not for ophthalmic Rx laboratories, not a bench tool for polishing spectacle lenses, and not for architectural glass or mirror work. If that is the job, we are the wrong supplier and would rather say so before you send a drawing.
Where an optical lens polishing machine sits in the line
Polishing is one station of six, and it inherits whatever the station before it left behind.
- Before: the radius is cut on a curve generator. Allowance and subsurface damage from that step decide how long fine grinding takes here.
- After: the finished faces go to edging and centering, where the outside diameter is brought to the optical axis.
- Alongside: the damage story is worth reading in full — see our note on subsurface damage in optical lenses, which is what this step exists to remove.
- All of it together: the complete lens fabrication line, laid out as one proposal with cycle times, or browsed by process step on the equipment overview.
An optical lens polishing machine bought without looking upstream tends to disappoint: if the generator leaves an uneven allowance, the polishing cell spends its cycle correcting damage instead of figure. Tell us both steps and we will balance them.
What do buyers ask before they choose?
Do fine grinding and polishing need two machines?
Not two frames. The same optical lens polishing machine runs both, configured for one or the other — what changes is the tooling and the consumables, so shops with volume often buy two identical frames and dedicate one to each stage.
Can one frame do concave and convex?
No. Upper swing is built for concave, lower swing for convex. A mixed part programme means either two frames, or the tilt-axis machine where the geometry is set differently.
How many lenses per cycle?
Four or six on a swing frame, one per spindle. For flat parts, a double-sided machine runs a whole carrier set at once — which is why an optical lens polishing machine for wafers is specified by plate size, not spindle count.
What about ceramics and sapphire?
They need metered slurry rather than a flood, and pressure that stays put as the tool wears. That is the FP-6X with its drip-feed option; glass work stays on the circulating pump.
What has to be quoted besides the machine?
Tools and fixtures for your radii, the first set of consumables, destination voltage and CE configuration, freight, installation and training, and a spare-parts set. An optical lens polishing machine is a tooling-heavy purchase — budget it as a cell, not a frame.
Can these machines be loaded automatically?
Basket loading units feed the polishing station directly from the generating cell. They are specified with the line so basket and tray formats match at every station, rather than retro-fitted afterwards.
Send the lens — get a machine recommendation
You do not have to land on a model number yourself. Send the drawing, the material and the annual quantity, and you get back a specific machine, a cycle estimate and trial parts to check it against.
- 1 · You send — drawing or sample, material, radius and sign, batch size.
- 2 · We answer — frame, swing direction, tooling and an estimated cycle time.
- 3 · We prove it — free trial run on your own blanks, parts returned with the process sheet.
- 4 · You decide — firm quotation including tooling, consumables, freight, installation and training.