
Prism Faceting Machine MF-3
A prism faceting machine that rough-grinds, fine-grinds and polishes an optical polyhedron in one machine. Two workpiece spindles index layer by layer and face by face under servo control, so each flat lands at its set angle without the part ever leaving the fixture.
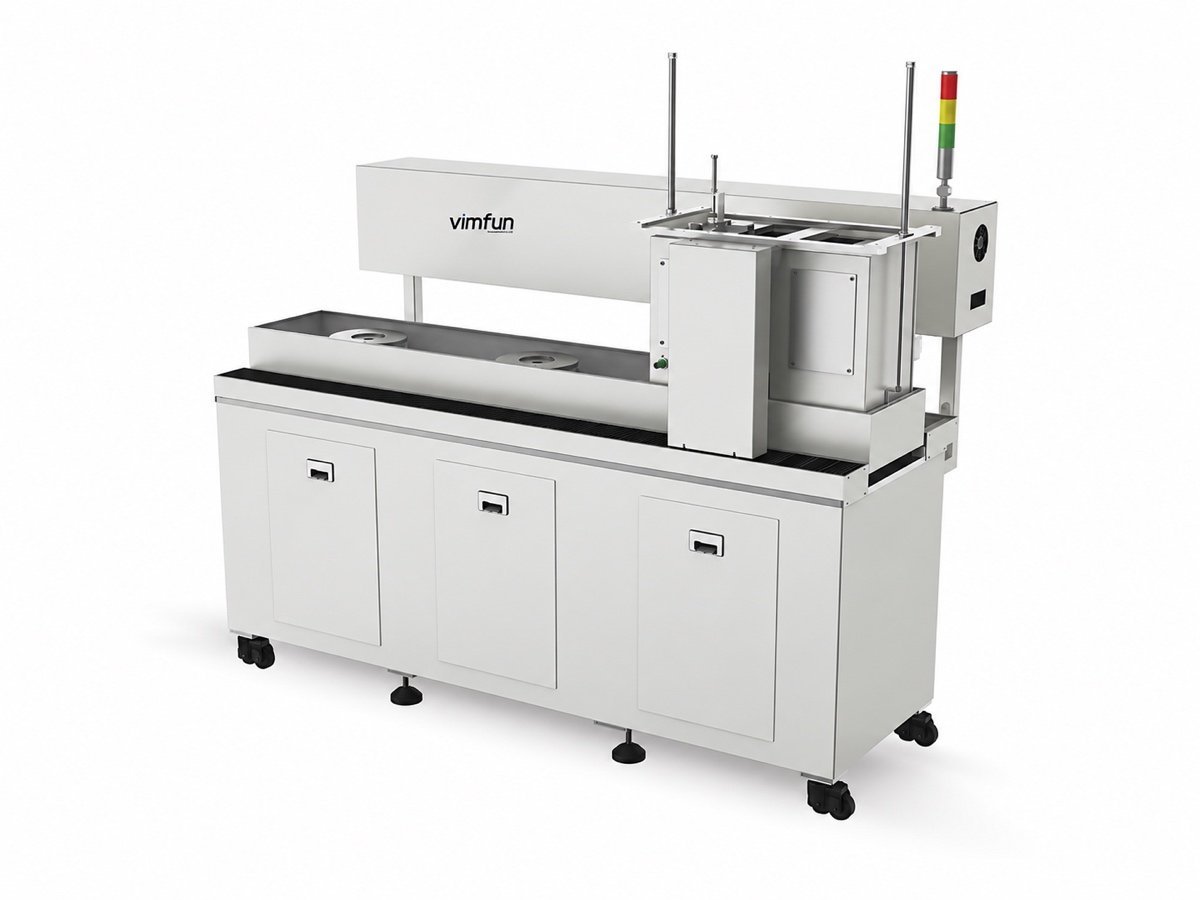
Flats and angles, not spheres — how it differs from the FP polishers
The FP polishers on this line finish curved surfaces: a workpiece swings about a sphere centre and a spherical face comes off it. The MF-3 does the opposite geometry. It grinds and polishes the flat faces of a polyhedron — a prism, a wedge, a many-sided optical block — by indexing the part to each angle and bringing a flat plate up to it. So a prism faceting machine brings a polyhedron to size, angle and finish, where a spherical polisher would have nothing curved to work.
Because the MF-3 carries all three stages — rough grind, fine grind and polish — on one bed, a faceted part does not move between machines. Where the job is a spherical lens instead of a flat, the concave FP-4U polisher and convex FP-4L polisher are the right machines; the MF-3 is the one built for flats and angles.
What a prism faceting machine is for: the flat faces of a multi-sided optical part, rough-ground, fine-ground and polished in one clamping. It does not generate or polish a spherical surface — that is the FP series, and this page links to it.
How does a prism faceting machine hold every angle?
By indexing the part in two directions — layer and face — under servo control, and letting a flat plate rise to meet each face in turn, so the angle is set by the machine and not by the operator’s hand.
The part is glue-fixed to a workpiece spindle. Two servo axes index it: one steps through the layers of faces, the other steps from face to face within a layer. Below it sits a machining plate that rises to touch the part. The grinding feed is numerically controlled, which is what holds the size; the polishing feed is a flexible force feed with torque monitoring, which is what keeps the finish even.
What that buys you:
- Servo layer and facet indexing — the two indexing axes are servo-driven, so every face returns to its set angle rather than being aligned by eye
- Three plates on one bed — rough-grind, fine-grind and polish plates in sequence, the part moving between them on a gantry table
- NC grind feed, flexible polish feed — the grind feed is numerically controlled for size; the polish feed is force-controlled and torque-monitored for finish
- Zero-point plate compensation — the polish plate wears thinner with use; a zero-calibration device measures it and compensates automatically
Because a prism faceting machine indexes the part and runs all three plates from one program, the operator loads and unloads and the machine does the sequencing — which is where the angle repeatability comes from.
The fixture and the face program are made to your part and its angle scheme. Send us the part, the faces you need and the material, and we specify the fixture and the cycle with the quotation.
Four things the machine does on its own
Loading and unloading is by hand; the grind, the fine grind and the polish of every face run from one program. These are what a prism faceting machine gets right.
Whole cycle on one bed
Rough grind, fine grind and polish happen on three plates in sequence, the part carried between them, so a faceted block is finished without moving to another machine.
Servo angle, layer and face
Two servo axes index the part — layer by layer, face by face — so each flat returns to its set angle part after part, which is what a hand-indexed lap cannot promise.
Compensates plate wear itself
Before polishing, a zero-point device measures the polish plate, which thins as it works, and compensates for it — so the surface figure does not drift as the plate is consumed.
Enclosed, waterproof, washable
The working zone is stainless behind guards, waterproof and easy to wash down between jobs, on a fully welded base.
Which parts and materials can it face?
| Item | Capability |
|---|---|
| Work done | Rough grind, fine grind and polish of flat faces |
| Part type | Prisms, wedges and other optical polyhedra; symmetric and asymmetric faces |
| Max range | Diameter / diagonal Ø110 mm, thickness 30 mm |
| Fixing | Workpieces glue-fixed to the spindle |
| Materials | Optical lenses and other optical materials — send yours for a free trial run |
A prism faceting machine is judged on face angle, flatness and finish, so those are the numbers to send with the part. If you are choosing glass, the optical materials data helps, and drawings dimensioned to the ISO 10110 framework are ideal for a faceted part.

Technical specifications
The MF-3 facets flats and angles; the FP series polishes spherical faces, which is a different geometry.
| Work done | Rough grind, fine grind, polish of flat faces |
| Max machining range | Diameter / diagonal Ø110 mm |
| Max machining thickness | 30 mm |
| Workpiece spindles | 2 |
| Machining plates | 3 — rough grind, fine grind, polish |
| Plate diameter | Ø260 mm |
| Grind / polish spindle runout | < 0.02 mm |
| Swing-frame oscillation | 0 – 30 cpm, stepless |
| Swing range | 0 – 50 mm |
| Indexing | Layer and facet, servo, PLC control |
| Grind feed / polish feed | NC grind feed; flexible polish feed, torque-monitored |
| Spindle motors | 3 × 2.2 kW |
| Total installed power | approx. 7.5 kW |
| Overall dimensions (L × W × H) | 2000 × 800 × 1700 mm |
| Total weight | approx. 750 kg |
| Base construction | Fully welded |
Face-angle, flatness and parallelism targets are set against your part and confirmed on the quotation, not published as a single figure — they depend on the material, the face scheme and the tolerance you have to hold.
Main assemblies and what each one is for
This is the vocabulary your operator and our service engineer will share on the shop floor.
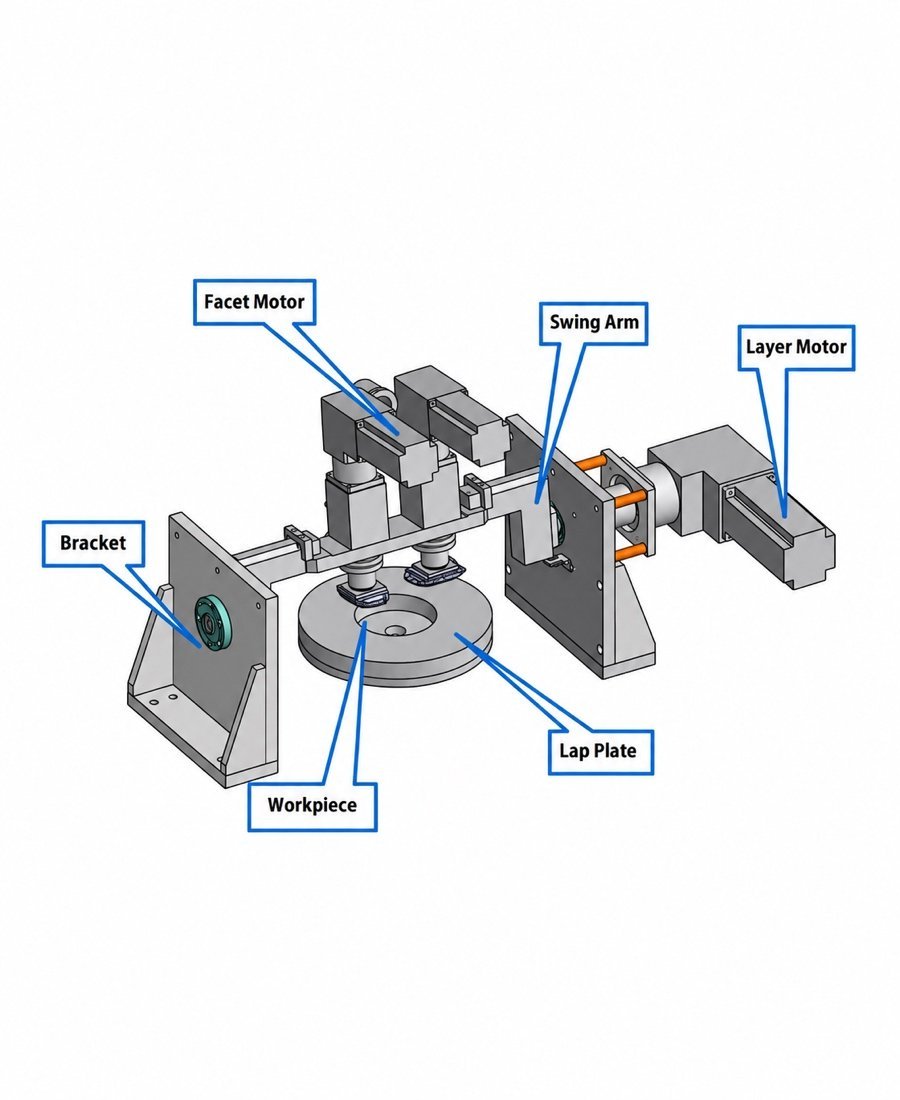
| Assembly | Function |
|---|---|
| Workpiece spindles (×2) | Hold the glue-fixed parts; carry the layer and facet indexing |
| Facet motor | Servo motor that steps the part from face to face within a layer |
| Layer motor | Servo motor that steps the part through the layers of faces |
| Swing arm | Oscillates the work over the plate, stepless 0–30 cpm |
| Gantry worktable | Motor-driven table that moves the work between the grind and polish plates |
| Machining plates (×3) | Rough-grind, fine-grind and polish plates; each rises to meet the face |
| Zero-point calibration device | Measures polish-plate wear and compensates for it automatically |
| Operation panel | PLC control for the program, the indexing and the feeds |
Utilities, environment and safety
Electrical supply, compressed air, coolant, floor loading and the ambient conditions the machine is to run in are confirmed with us for each order, together with the safety and protective arrangement supplied with it. These figures depend on the voltage and frequency of your site, the material you are running and the destination market, so we do not publish a single set of them here.
Send us the site conditions with your enquiry and we will return the utility and environmental requirements in writing, before the order is placed.
The MF-3 grinds and polishes flat faces on optical polyhedra — it does not generate or polish a spherical or cylindrical surface, and it is built for precision optical polyhedra to a drawing. A new part needs its fixture made and its face program proven on trial parts, the reason we ask for your parts before quoting.
What happens after the machine is installed?
The same terms apply to every machine we ship, wherever in the world it goes.
| Warranty period | 12 months from final acceptance |
| Response during warranty | Response within 8 hours · solution proposed within 24 hours · issue resolved within 48 hours, including procurement, installation and commissioning of parts |
| After the warranty period | Service and spare parts available for the life of the machine |
| Certification | CE |
Specifications are subject to change as a result of design upgrades. Minor differences may occur at certain parts. For a binding specification, refer to the order confirmation.
See the machine running
The MF-3 indexing a polyhedron face by face, and the plates rising through the grind, fine-grind and polish sequence.
01 — Faceting one polyhedron
02 — Through the three plates
Send one drawing and a few blanks
A prism faceting machine is easy to specify badly from a datasheet. Send us the part, the face scheme and angles, the material and the tolerance you have to hold, with a few of your own blanks. We run them, return them, and send the process sheet with the quotation.
If your job is a spherical lens rather than a faceted flat, we will point you to the FP polishers instead of quoting this one.
12-month warranty · free trial run on customer-supplied material
Optics customers include Edmund Optics and Coherent
Related equipment and reading:
- Concave lens polishing machine FP-4U — spherical concave faces
- Convex lens polishing machine FP-4L — spherical convex faces
- Tilt axis lens polishing machine FP-6X — flats and spheres, tilt axis
- Optical lens fabrication line — how the stations connect