
Quartz Grinding Machine
Two materials share the name. A quartz grinding machine set up for fused silica will chip crystal quartz at the rim, because one is a glass and the other is a single crystal with directions that matter.
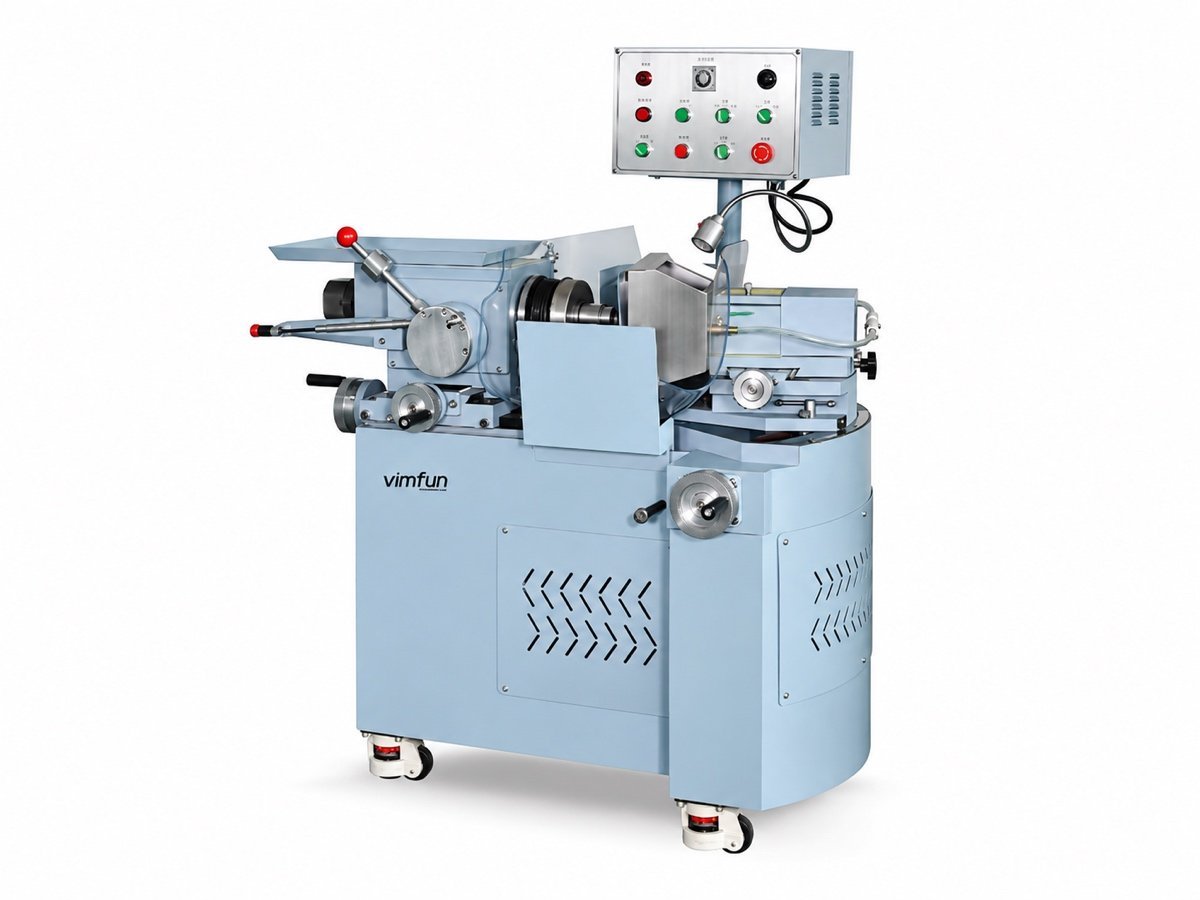
Fused silica and crystal quartz are two different jobs
Both are SiO₂ and that is where the similarity ends. Get this distinction wrong on the shop floor and you will blame the machine for a material problem.
Fused silica cracks from heat
It tolerates almost any grinding direction but very little thermal shock at the contact zone. Coolant that is merely present is not enough — it has to arrive where the wheel is working, which is why large work moves to internal-jet delivery.
Crystal quartz breaks along planes
Cut and ground in the wrong direction it chips at the rim no matter how gently you feed. The fix is upstream: the slicing orientation, and a chamfer before the rim ever sees a grinding wheel.
Both load the wheel fast
Quartz is harder on abrasive than optical glass. Expect a shorter dressing interval than the same wheel gives on optical glass, and plan the consumable budget on that basis rather than on a glass benchmark.
The practical consequence is a quoting problem, not a physics problem. A drawing that says only “quartz”, with no grade and no cut, forces us to guess the fixture, the wheel grade and the chamfer strategy — and a guess is what turns into scrap on your first production batch. Two extra lines on the drawing remove all of that risk before anyone quotes anything.
Before any quartz grinding machine is quoted, we need to know whether the part is fused silica or crystal quartz, and for crystal, which cut. Published data such as Crystran’s crystal quartz sheet is a useful cross-check when the drawing is silent.
Which quartz parts and formats does it cover?
Every quartz grinding machine in this range is built for optical work rather than semiconductor volume: windows, lenses and blanks, not 300 mm wafer lines.
| Part | Typical format | Which station does the work |
|---|---|---|
| Windows and flats | Flat, both faces parallel, to Ø395 mm | Double-side lapping, then edge work |
| Spherical lenses | Convex, concave, R2 to flat, Ø4–120 mm | Curve generating, then spherical-centre polishing |
| Discs and blanks from ingot | Sawn slices, cored discs | Wire saw first, generating second |
| Rods and cylindrical parts | Round bar stock, sliced to length | Slicing, then flat generating on the faces |
- Thickness control in-process sagitta measurement with automatic compensation holds centre thickness across a batch as the wheel wears.
- Parallelism on windows comes from batch lapping between two plates, not from machining one face at a time.
- Drawing language tolerances written to ISO 10110 tell us which of these stations your tolerance actually depends on.
- What we do not do no crucibles, tubing or fused-quartz ware, and no semiconductor wafer thinning lines.
How does a quartz grinding machine fit after the saw?
On quartz the saw matters more than on glass, because orientation and kerf are decided there. The quartz grinding machine inherits whatever the saw left: stock to remove, and a rim that is either chamfered or already chipped.
Where the four stations are bought together, the trays and batch sizes line up and a part never waits for a fixture to be made — the argument is set out on the complete fabrication line page. Material behaviour across the range is collected on optical lens materials.
What goes wrong on quartz, and what stops it?
Four of these five are specific to quartz. Working through them before the quartz grinding machine is chosen is cheaper than working through them on your own blanks afterwards.
| Defect | Where it starts | What stops it |
|---|---|---|
| Thermal cracking | Fused silica, heat at the contact zone on heavy stock removal | Coolant delivered through the wheel, lighter infeed, no dwell at breakthrough — see the SG-120 on large work |
| Rim break-out | Crystal quartz cut or ground across its fracture planes | Orientation fixed at slicing, chamfer before generating, supported fixturing |
| Subsurface damage | Coarse or glazed wheel during generating | Finer grade and a kept dressing schedule; polish removal deeper than the damaged layer — background in our note on subsurface damage |
| Wheel glazing | Quartz loading the bond faster than on glass | Shorter dressing interval, in-cycle dressing where the machine has it |
| Thickness and TTV spread | Windows machined one face at a time | Batch lapping between two plates on the DL-290/395, which holds the batch rather than the part |
One more item that is not strictly a defect but costs the same money: quartz swarf is abrasive and stays in suspension longer than glass swarf. Coolant filtered on a complaint schedule rather than a calendar will put scratches into parts the grinding wheel never touched.
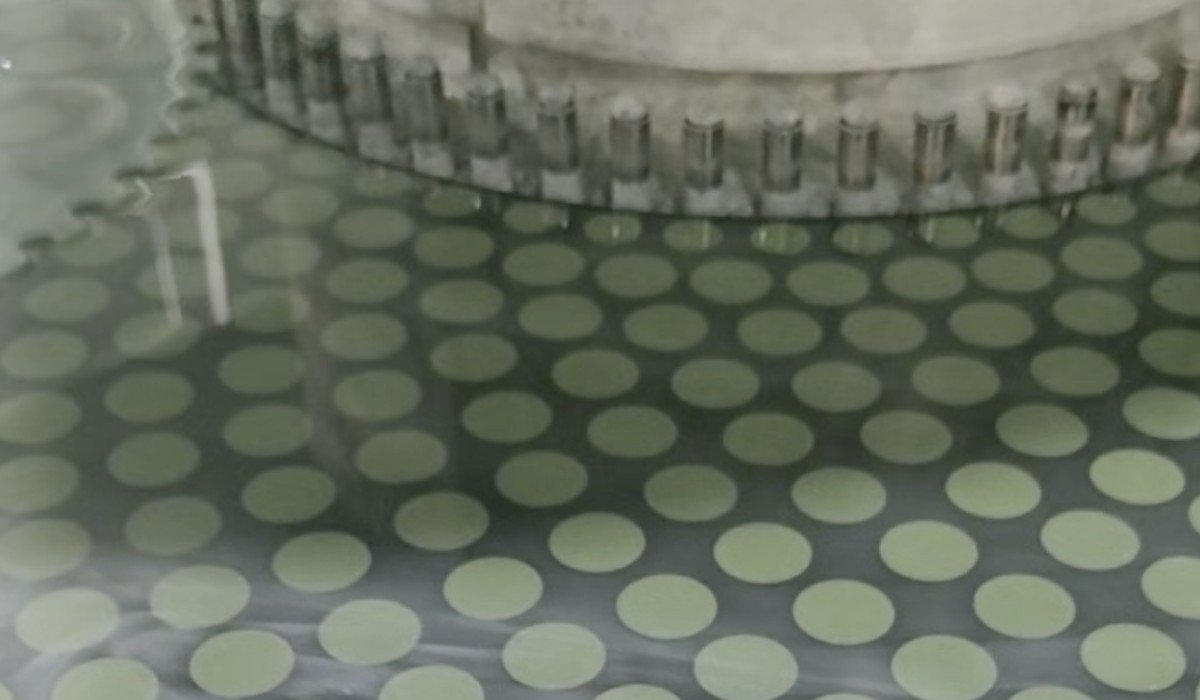
Curve generating or double-side lapping for your quartz?
The part decides, not the material. Anything with a radius goes to a generator and then to spherical-centre polishing. Anything flat where both faces have to stay parallel — windows, wave plates, optical flats — belongs on a double-side lapping machine, where the batch is held between two plates and every part in the load sees the same pressure.
The mistake we see most often is a shop machining flat quartz windows one face at a time on a generator because that is the quartz grinding machine they already own, then fighting parallelism in final inspection every single batch.
Batch size decides the fixture bill as well. Lapping carriers are cut for a diameter and a thickness band, so a shop with three window sizes buys three sets — better priced into the quotation than discovered in the second month of production.
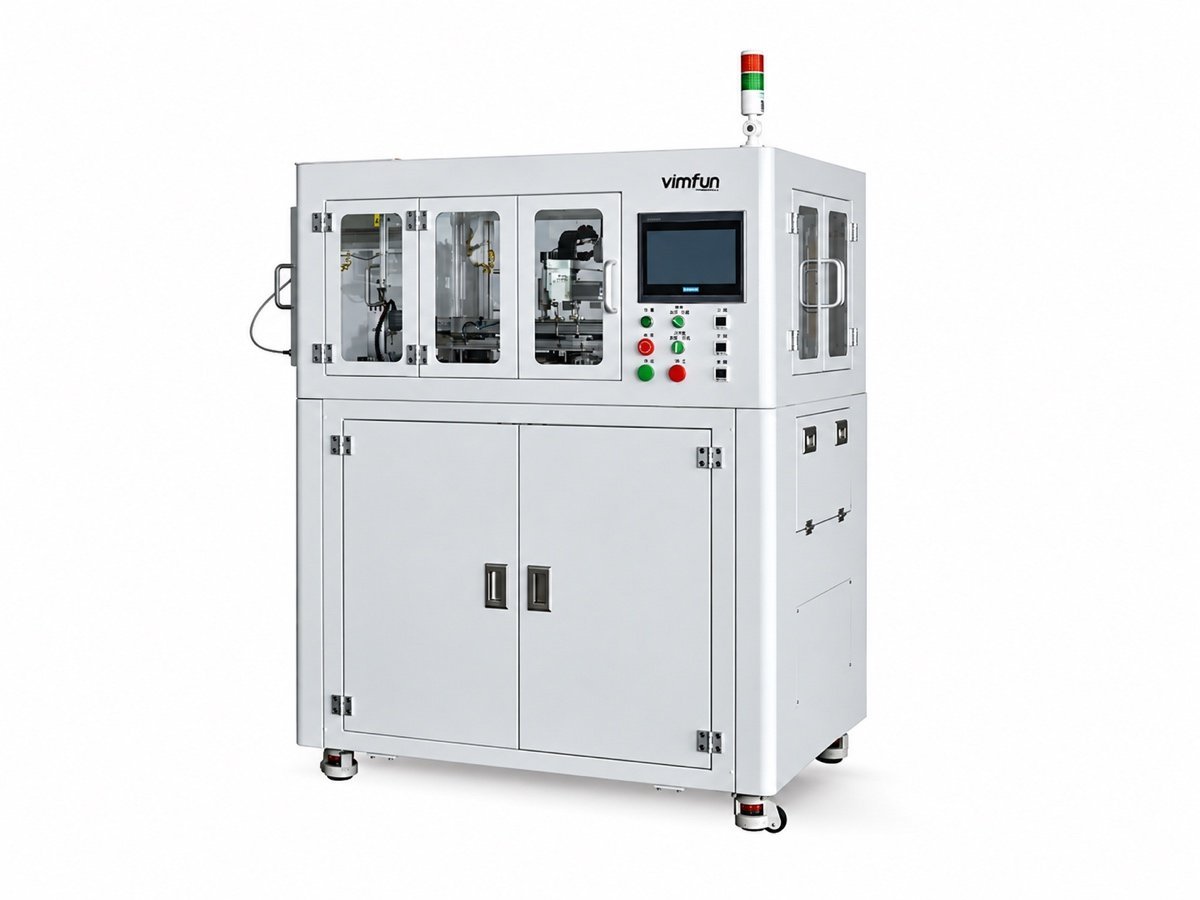
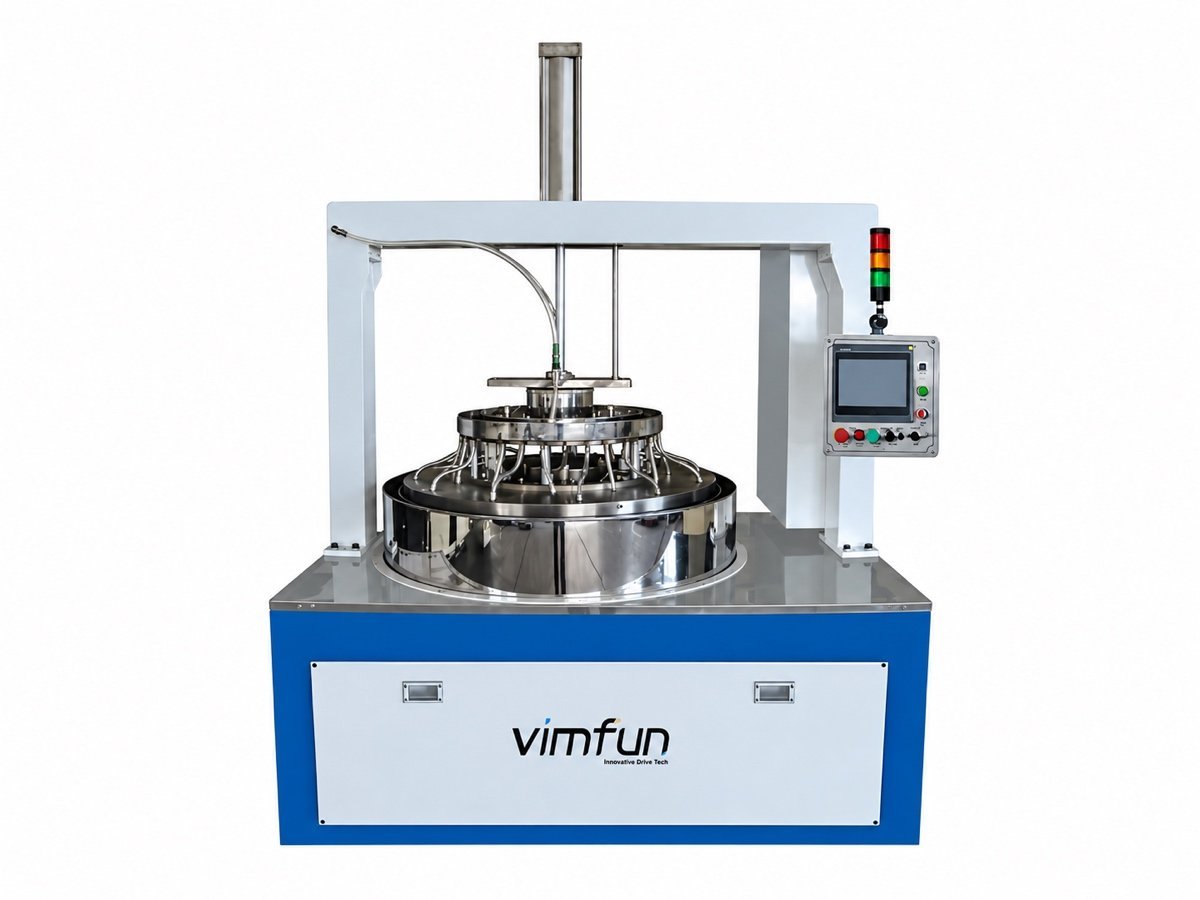
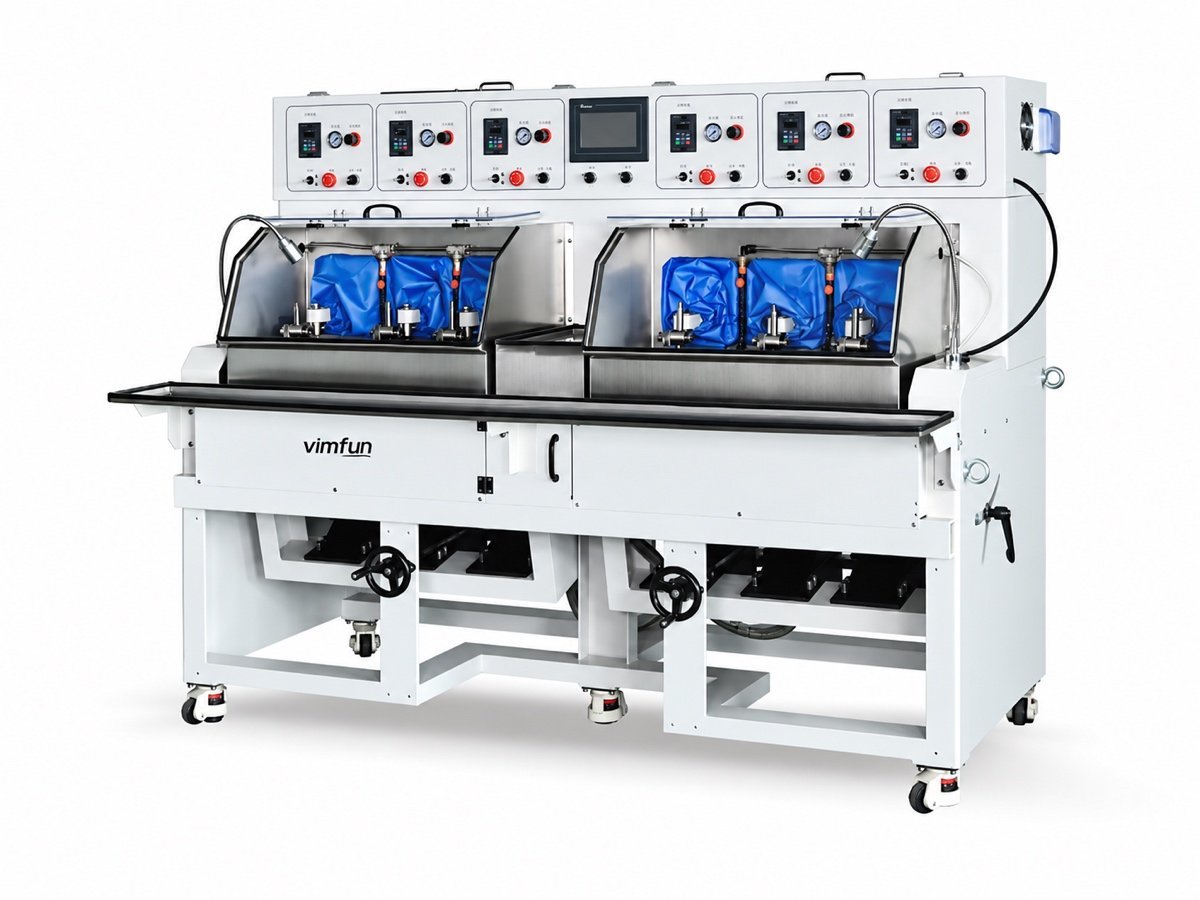
The full selection matrix by diameter, curvature and loading method is on the optical lens grinding machine page; the fine grinding and polishing side is on the polishing range. Sister material pages: optical glass, ceramics and optical crystals; what drives the quotation is on the price page.
Send the quartz, and say which quartz it is
We run your own blanks on the matching machine, free, and report what happened — cycle time, rim condition and what we would change. It is the only honest way to specify a quartz grinding machine.
Arrange a trial run- Fused silica or crystal quartz — and for crystal, which cut
- Flat or radiused, and the tolerance that matters most
- Diameter, thickness and batch size
- Whether the blanks arrive sawn, cored or as ingot
Free trial run on your own blanks, freight at your cost · ISO 9001 · CE · 12-month warranty · 8-hour response