
Spherical Lens Curve Generator SG-80
A manually operated spherical lens curve generator that grinds a convex, concave or flat surface into one blank at a time, up to Ø80 mm. The operator sets the tilt, runs the cut and checks the sagitta by hand. Optical glass, sapphire, ceramics and crystal.
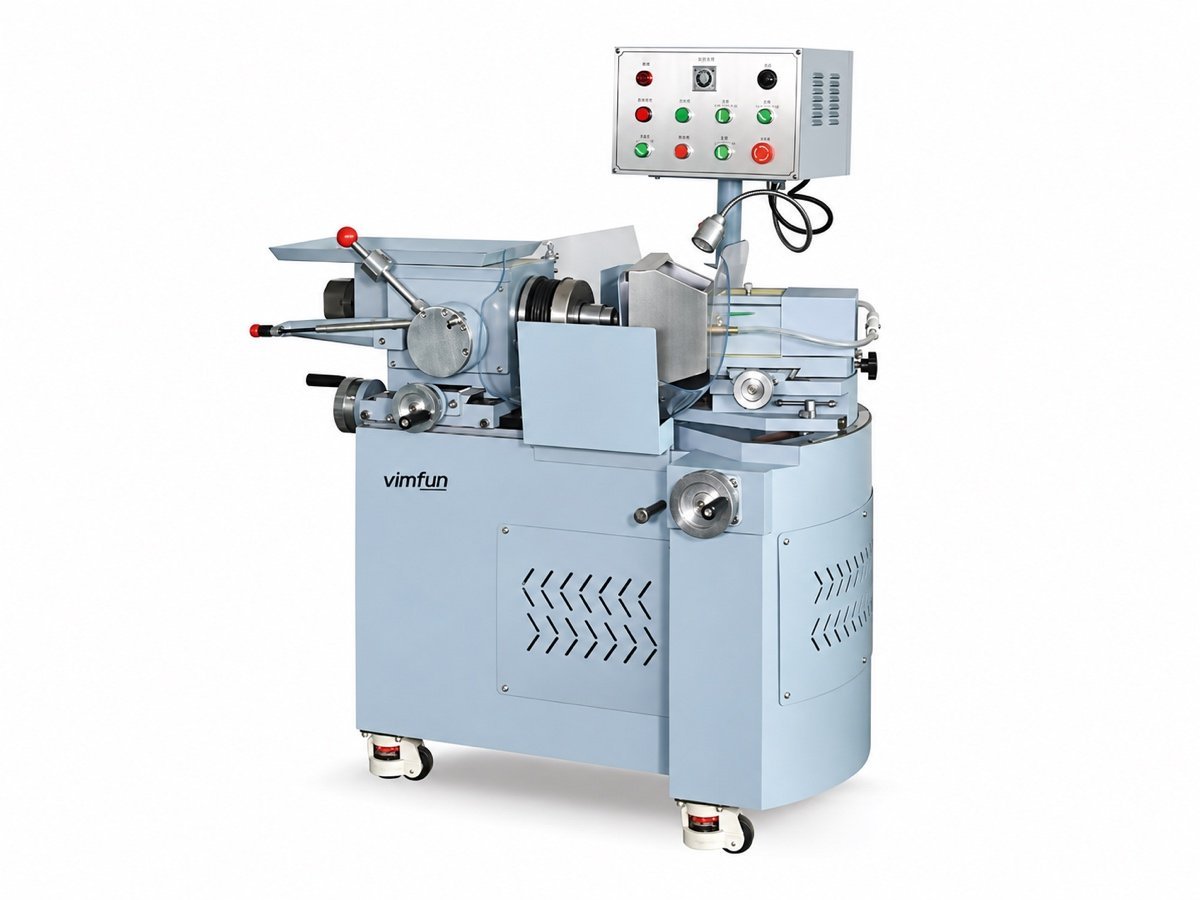
What this machine makes, and what happens before and after it
An optical element starts as a sawn or pressed blank and ends as a coated, centred lens. A spherical lens curve generator owns one step in the middle: it cuts the radius of curvature into the face of the blank and brings the centre thickness close to the drawing. The SG-80 is the manual member of that family — everything upstream supplies it, everything downstream inherits the surface it leaves.
The part that leaves this machine is not finished. Its radius and centre thickness are close enough to specification that the lapping and polishing stage removes microns rather than re-cutting the curve. On a manual machine that outcome rests on the operator, which is exactly what this page is about.
Think of this machine as the one that decides what shape the lens is. The machines after it decide how smooth it is. On the SG-80 a person, not a program, sets that shape.
How does a spherical lens curve generator cut a radius?
No template, no copy former, no profile cam. On this class of machine the radius comes out of an angle — and on the SG-80 that angle is set by hand.
Two spindles do the work. The tool spindle carries a diamond cup wheel — a ring whose rim is charged with diamond grit — and turns it at 8,000 or 11,000 rpm. The workpiece spindle holds the blank, rotates it slowly at 0–36 rpm and feeds it against the wheel while the operator watches the cut.
Because the cup wheel is tilted, its circular cutting edge sweeps out a sphere as the blank turns underneath it. The radius of that sphere is fixed by geometry alone:
- sin θ = d / (2R) — where θ is the spindle tilt, d the effective cutting-edge diameter of the cup wheel, and R the radius produced
- θ = 0° — the two axes are parallel and the machine generates a plane
- tilt 0–45° — the steeper the setting on the rotating carriage, the shorter the radius produced
- Convex or concave — decided by which side of the workpiece axis the wheel is tilted to
Set the carriage angle once and every part comes out with the same radius. This is why a spherical lens curve generator has no tooling to swap between one radius and the next — only the angle and the wheel change.
You are not buying a fixed set of radii. You are buying a range set by the 0–45° carriage and the wheels that suit your materials. Send us the radii you need and we will specify the wheels with the quotation, not after it.
What does the operator decide on a manual machine?
The SG-80 has no sagitta feedback loop and no automatic loader. On a manual spherical lens curve generator those decisions stay with the person at the machine — which is why an experienced operator gets more out of it than a datasheet suggests.
Sets the carriage angle and reads the first part
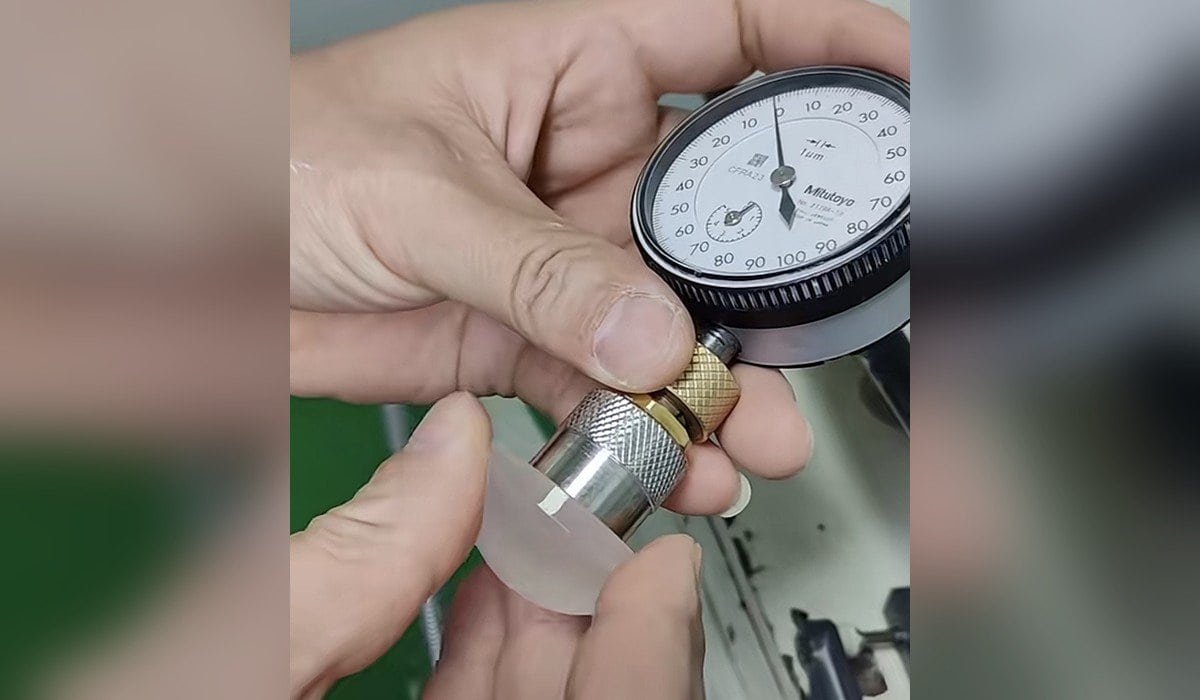
The rotating carriage is set to the tilt the radius calls for, a trial part is cut, and its sagitta is measured off the machine. The operator adjusts the setting until the reading matches the drawing, then locks it for the run.
Chooses the spindle speed for the material
The tool spindle runs at 8,000 or 11,000 rpm. The faster step suits smaller diameters and harder substrates; the operator picks the pairing of speed and feed the blank can survive without edge chipping.
Feeds by hand and watches the wheel
Stock is taken off in a fast approach and progressively lighter passes. A person feeding the workpiece spindle feels the cut and eases off as the surface comes up — the judgment a five-stage servo program automates on the CNC machines.
Dresses the wheel when the cut tells them to
When the cut slows or the finish coarsens, the operator trues the cup wheel and, if needed, re-checks the sagitta. Catching wheel wear early is the skill that keeps a manual run consistent part to part.
If these four decisions have to hold across a long unattended run, the CNC member of this family does them in-cycle. See the CNC optical curve generator Auto-SG-50, which measures the sagitta, compensates the feed, flips the part and loads from a tray on its own. The SG-80 is the machine for setup work, short runs and prototyping; the Auto-SG-50 is the machine for volume.
Which materials and geometries can it handle?
| Item | Capability |
|---|---|
| Surfaces generated | Convex and concave spherical surfaces; plane (flat) surfaces |
| Radius range | Set by the rotating carriage, tilt 0°–45°; flat at 0° |
| Workpiece diameter | Up to Ø80 mm |
| Workpiece stroke | 70 mm |
| Workpieces per cycle | 1 — single-part, manual load |
| Materials | Sapphire, optical glass (crown / flint), technical and optical ceramics, and crystal |
| Surface-form accuracy | ≤ 0.003 mm |
| Centre-thickness error | ≤ 0.01 mm |
| Chamfering | Chamfer device, tilt 0°–45° |
If your drawings are dimensioned to the ISO 10110 framework, send one with the enquiry. The radius tolerance and centre-thickness tolerance on that drawing are what decide whether a manual spherical lens curve generator is right for the job, or whether the run belongs on the CNC version — not the material.
Technical specifications
For larger work up to Ø120 mm, the SG-120 shares this architecture with added spindle power and internal wheel cooling.
| Max machining diameter | Ø80 mm |
| Workpiece stroke | 70 mm |
| Rotating carriage tilt | 0° – 45° |
| Chamfer device tilt | 0° – 45° |
| Tool spindle speed | 8,000 / 11,000 rpm |
| Workpiece spindle speed | 0 – 36 rpm, stepless |
| Tool spindle runout (radial / axial) | ≤ 0.005 mm |
| Workpiece spindle runout (radial / axial) | ≤ 0.005 mm |
| Two-axis height match | ± 0.25 mm, adjustable |
| Surface-form accuracy | ≤ 0.003 mm |
| Centre-thickness error | ≤ 0.01 mm |
| Spindle motor | 1.1 kW × 2 poles |
| Workpiece motor | 0.12 kW (1:40) |
| Overall dimensions (L × W × H) | 1.3 × 1.0 × 1.5 m |
| Total weight | approx. 600 kg |
| Base construction | Cast iron, hand-scraped mating surfaces |
On a spherical lens curve generator the diamond cup wheels and dressing stones are process consumables chosen for the material and the radius being generated. They are quoted separately from the machine — tell us your materials and radii and we will specify them.
Main assemblies and what each one is for
The SG-80 keeps a spherical lens curve generator down to the parts an operator actually touches. This is the vocabulary your operator and our service engineer will share on the shop floor.

| Assembly | Function |
|---|---|
| Tool spindle | Carries the diamond cup wheel at 8,000 / 11,000 rpm; belt-driven |
| Rotating carriage | Tilts the tool spindle 0°–45° to set the generated radius; locked for the run |
| Workpiece spindle | Holds and rotates the blank at 0–36 rpm stepless; hand feed against the wheel |
| Chamfer device | Separate 0°–45° device for edging the finished face |
| Coolant system | Circulating supply flooding the cut, tank in the machine base |
| Cast-iron base | Hand-scraped mating surfaces holding the two spindles to the ≤ 0.005 mm runout and ± 0.25 mm height match |
| Operator controls | Spindle-speed selection, feed and carriage lock within reach of the working position |
Utilities, environment and safety
Electrical supply, compressed air, coolant, floor loading and the ambient conditions the machine is to run in are confirmed with us for each order, together with the safety and protective arrangement supplied with it. These figures depend on the voltage and frequency of your site, the material you are running and the destination market, so we do not publish a single set of them here.
Send us the site conditions with your enquiry and we will return the utility and environmental requirements in writing, before the order is placed.
A manual spherical lens curve generator is only as repeatable as the operator running it. On a new material the right pairing of spindle speed, feed and carriage angle takes a few trial parts to settle — this is the main thing we work out with you during commissioning, and the reason we ask for your blanks before quoting.
What happens after the machine is installed?
The same terms apply to every machine we ship, wherever in the world it goes.
| Warranty period | 12 months from final acceptance |
| Response during warranty | Response within 8 hours · solution proposed within 24 hours · issue resolved within 48 hours, including procurement, installation and commissioning of parts |
| After the warranty period | Service and spare parts available for the life of the machine |
| Certification | CE |
Specifications are subject to change as a result of design upgrades. Minor differences may occur at certain parts. For a binding specification, refer to the order confirmation.
See the machine running
The SG-80 generating a spherical surface on optical glass, and the operator setting the carriage angle and checking the first part.
01 — Spherical generating cycle, optical glass blank
02 — Carriage setup, first-part sagitta check
Send one drawing and a few blanks
A spherical lens curve generator is easy to specify badly from a datasheet. Send us one element drawing — diameter, radius, centre thickness, material and the tolerance grade you have to hold — together with a few of your own blanks. We run them, return them, and send the process sheet with the quotation.
If your tolerances or volumes need a machine class we do not build, we will tell you that instead of quoting.
12-month warranty · free trial run on customer-supplied material
Optics customers include Edmund Optics and Coherent
Related equipment and reading:
- CNC optical curve generator Auto-SG-50 — the automated version of this machine
- Optical lens grinding machine range — all the generating machines compared
- Concave lens polishing machine — the lapping and polishing stage downstream
- Optical lens fabrication line — how the stations connect